
“Our reports are still manual.”
Map the equipment signals to production context, then identify a reliable path into the systems people use.
MANUFACTURING INTEGRATION & AUTOMATION
Buntop connects equipment, SCADA, historians and MES so plant teams can identify production losses, trust their data and take practical steps to improve performance.
Existing plants. New lines. Clear ownership. Local control.
FOUNDER’S PRIOR EMPLOYMENT EXPERIENCE
Brownfield improvement combining edge integration, sensing and better production data.
Founder-reported prior employment result. This was not a Buntop client engagement.
Read the full improvement example ↗A FAMILIAR PROBLEM?
Map the equipment signals to production context, then identify a reliable path into the systems people use.
Review event quality, timestamps and asset context before building more dashboards.
Define the decision, assess the evidence, and establish human review and local safeguards.
01 / HOW WE HELP
Start with a defined problem and a focused assessment. Build toward a measured pilot and a supported rollout.
Understand how information moves today, where it breaks down, and what to improve first.
Test a useful connection on a limited scope before committing to a larger deployment.
Plan how a digital twin, maintenance model or optimizer could support people making plant decisions.
PHARMACEUTICAL & GxP MANUFACTURING
Start with intended use, quality ownership and a clear verification plan for equipment and instrument data.
See what an assessment delivers ↗
Each engagement has an agreed scope, deliverables and fee. Implementation follows assessment of your actual systems and site requirements.
BUILT AROUND REAL PLANT CHALLENGES
Beverage & packagingPharmaceutical, diagnostics & GxPAutomation delivery partnersSELECTED ARCHITECTURE EXAMPLES
Review three sanitized architecture examples. Each explains the problem, the proposed approach and the measurements needed to establish its impact.
Results not yet verified.
Review the design and evidence plan →Results not yet verified.
Review the design and evidence plan →Results not yet verified.
Review the design and evidence plan →Discuss the current systems, operating limits and evidence needed for your site.
SCOPED ENGINEERING SERVICES
A fixed-scope review of existing assets, data quality, ISA-95 structure and Purdue boundaries. Receive an interface inventory, risk register and prioritized roadmap.
Fixed fee after a short scoping call
Typically 2–3 assessment days, with report preparation and site access defined in the proposal.
One line, approved data interfaces, an edge-to-SCADA or broker path, and a dashboard verified against agreed acceptance checks.
Milestone-based proposal with agreed acceptance criteria
Milestone-based fixed fee. Hardware, licenses and travel are separately itemized.
Pilot proposals can include five named Academy seats for 12 months, with the learning tier, activation date and handover scope specified in the agreement. Team access is arranged with Buntop.
Ongoing design review, OT security oversight, change review and vendor quote assessment within agreed monthly capacity.
Monthly retainer based on agreed coverage
Coverage, response times and exclusions are agreed in writing.
Onsite commissioning and troubleshooting: Quoted by location, duration and technical scope. Travel, minimum booking terms and any hardware or license costs are itemized in the proposal.
Local control stays local. PLC interlocks, safety functions and equipment control remain under the plant’s local authority. Initial assessments use approved read-only interfaces; changes to active PLC logic require separate written scope, plant authorization, a maintenance window and a tested rollback plan.
02 / OUR APPROACH
A project is successful when the connection works, the evidence is clear, and your team can support it.
Agree on the production problem, current systems, baseline, constraints and decision owners.
Define interfaces, data context, storage roles, access boundaries and a limited first scope.
Agree on acceptance checks for data quality, failures, recovery and operating responsibilities.
Deliver documentation, review results with the plant team, and plan the next stage.
Supported interfaces. Least privilege. Clear system ownership. Local control. Documented validation.
OT security reviews cover risk assessment, vulnerability and patch planning, incident readiness, and operating policies, using IEC 62443 and NIST OT guidance where applicable.
03 / SEE THE APPROACH
Explore interactive architecture models that help teams review equipment data paths, system ownership, failure recovery and the evidence needed before implementation.
These simulations support design discussions and scenario checks. Site-specific engineering review and testing are required before implementation.
Review project experience and architectures →Public architecture summaries support early project discussions.
BROWNFIELD PROJECT
Identify existing PLCs, approved interfaces and local systems. Review data quality and access before proposing a limited integration.
04 / ENGINEERING EXPERIENCE
Adewale Adeniran Founder, Buntop Integrated Global Services LLC
Experience spanning electrical and controls engineering, manufacturing automation, onsite digital coordination and critical infrastructure.
Connect on LinkedIn ↗Cyber-Physical Systems · Indiana University Bloomington
University of Ibadan
Ladoke Akintola University of Technology
KRONES · Reyes Coca-Cola Bottling · bioMérieux · GE HealthCare · Nigerian Television Authority
These organizations reflect the founder’s professional experience, not a list of Buntop clients or endorsements.BEVERAGE & PACKAGING
Experience coordinating site teams, equipment connectivity, operator interfaces and the resolution of integration issues.
Read the experience example ↗DIAGNOSTICS MANUFACTURING
Experience with instrument integration, OPC UA and Kepware data paths, and Tulip MES workflows with quality and process owner review.
Read the experience example ↗A CLEAR STARTING POINT
A defined review of one production line or area, ending with a practical plan your engineering, operations and IT teams can use.
Equipment interfaces, SCADA, historian and MES responsibilities, data quality and access boundaries.
An architecture map, prioritized gaps, accountable owners and a pilot scope with acceptance checks.
Review the findings together, then agree on a focused pilot or implementation proposal.
FROM THE PLANT FLOOR
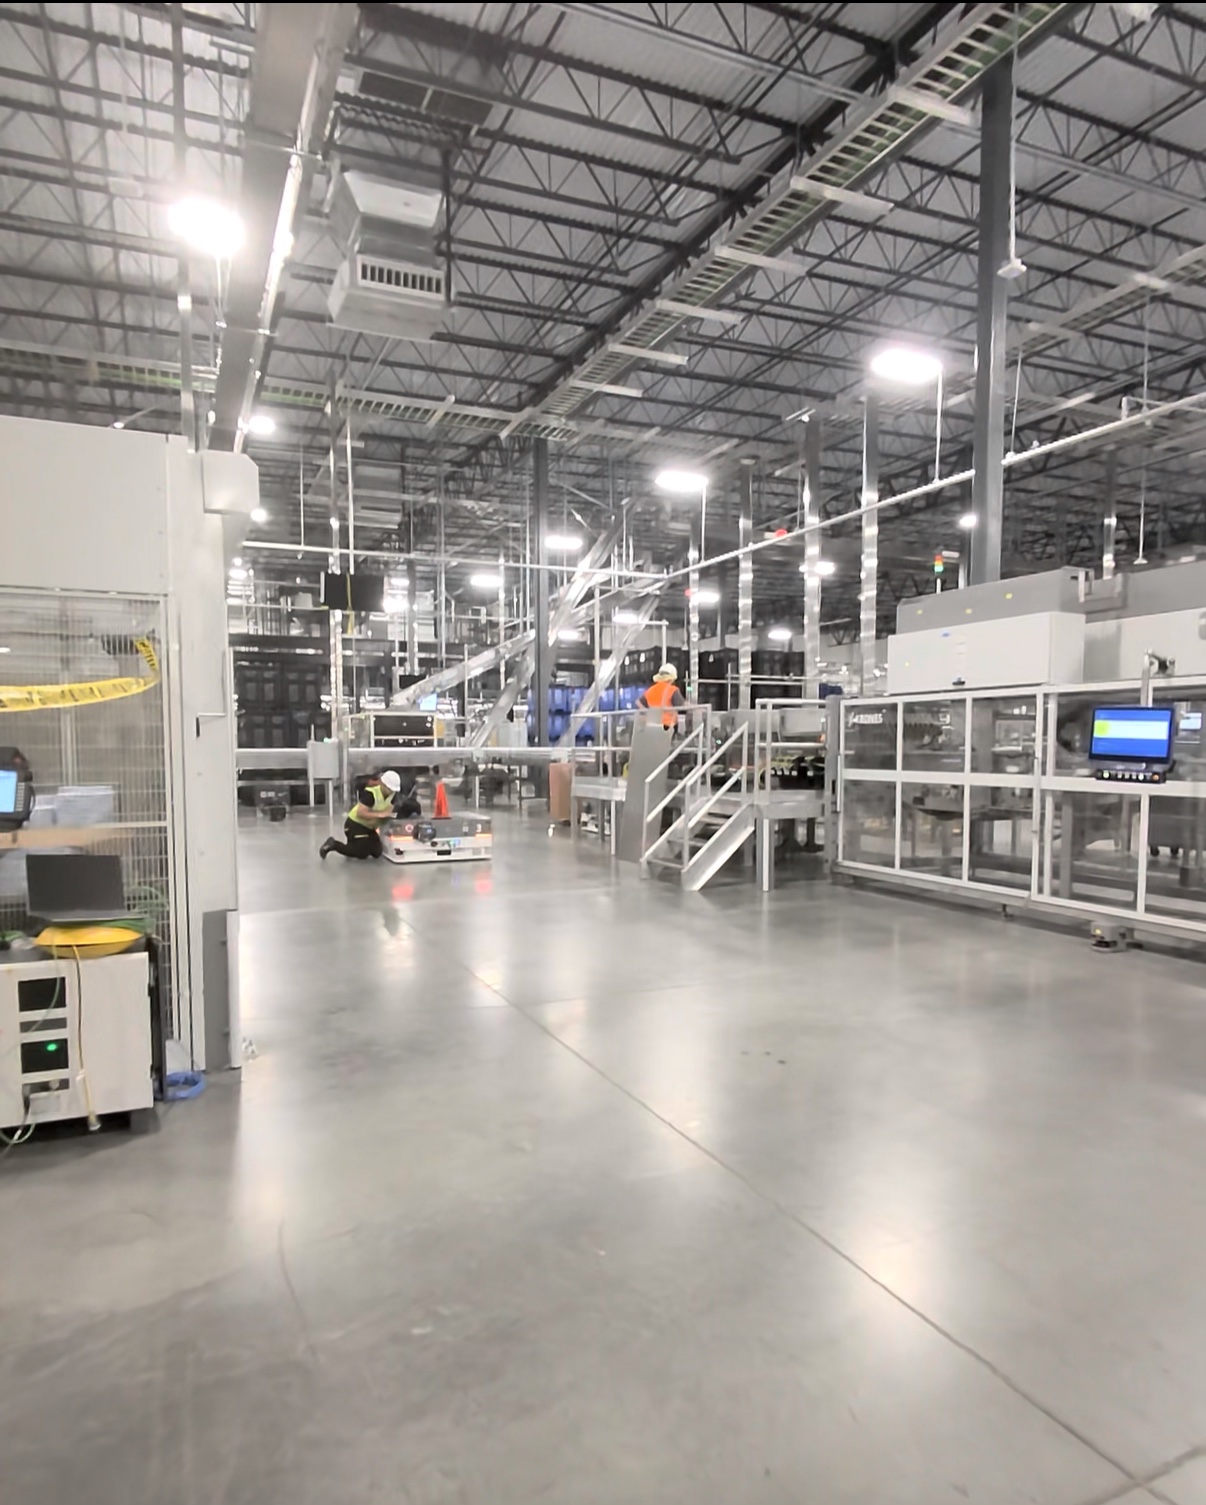
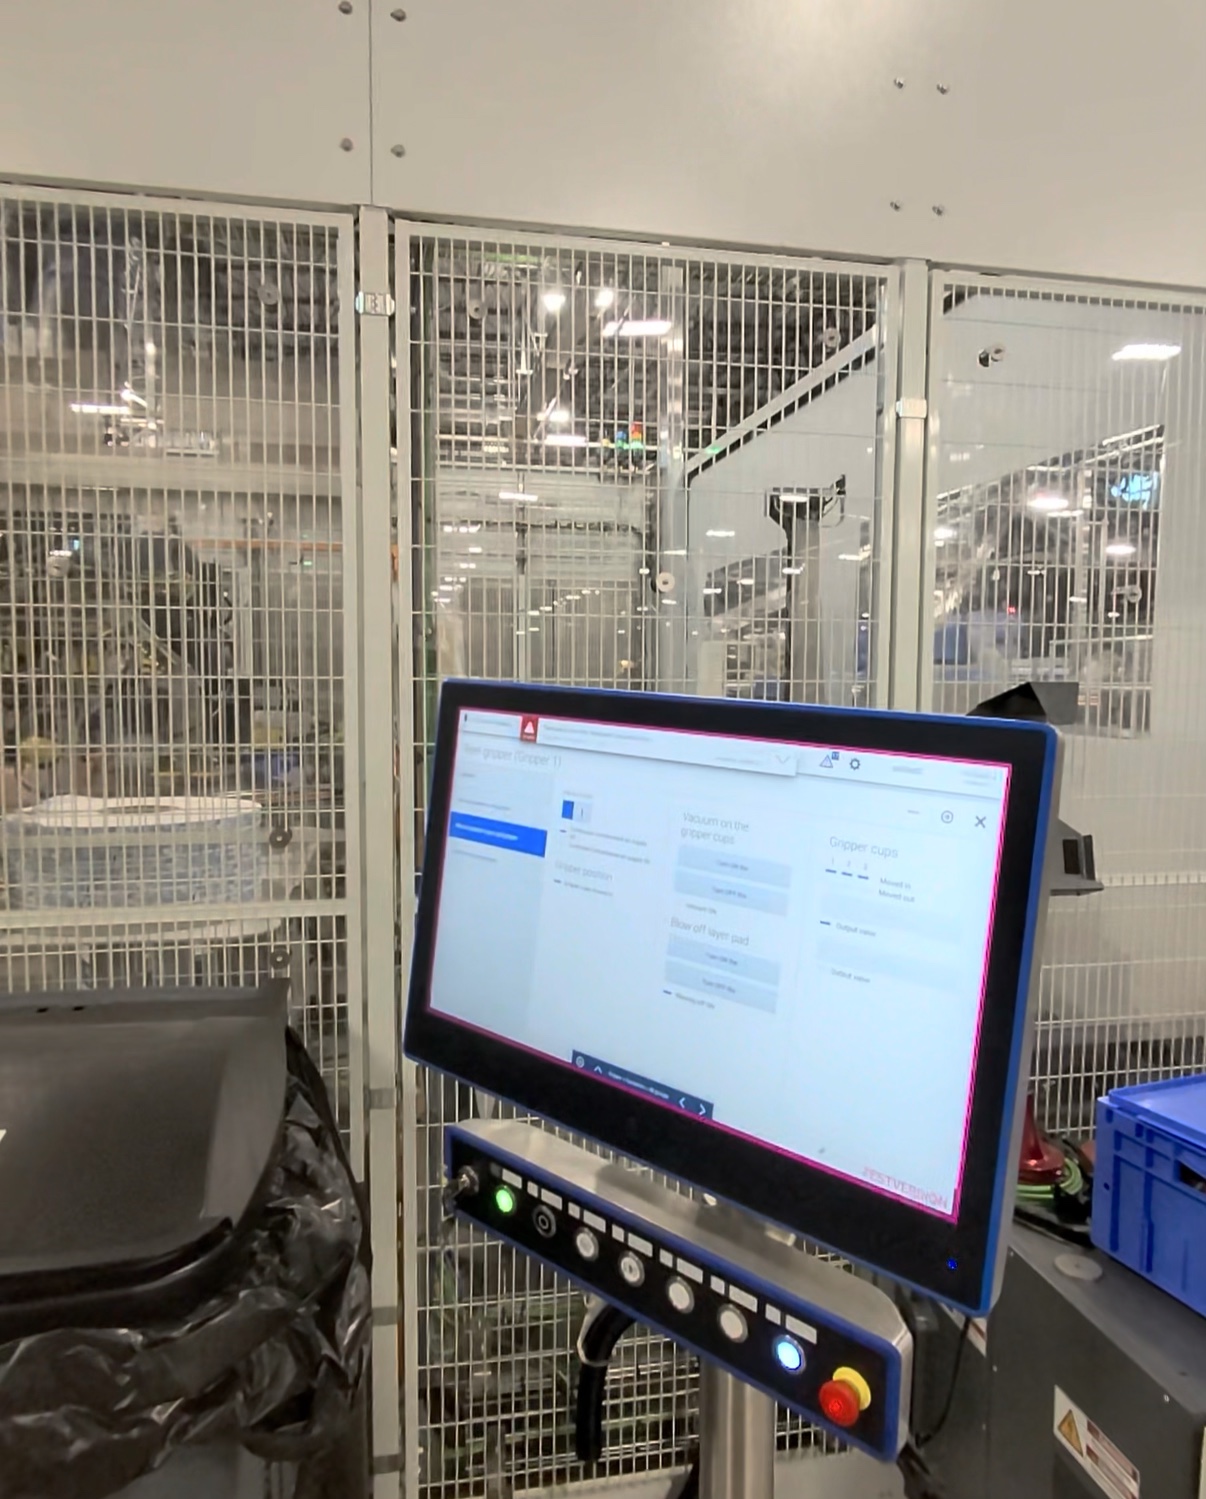
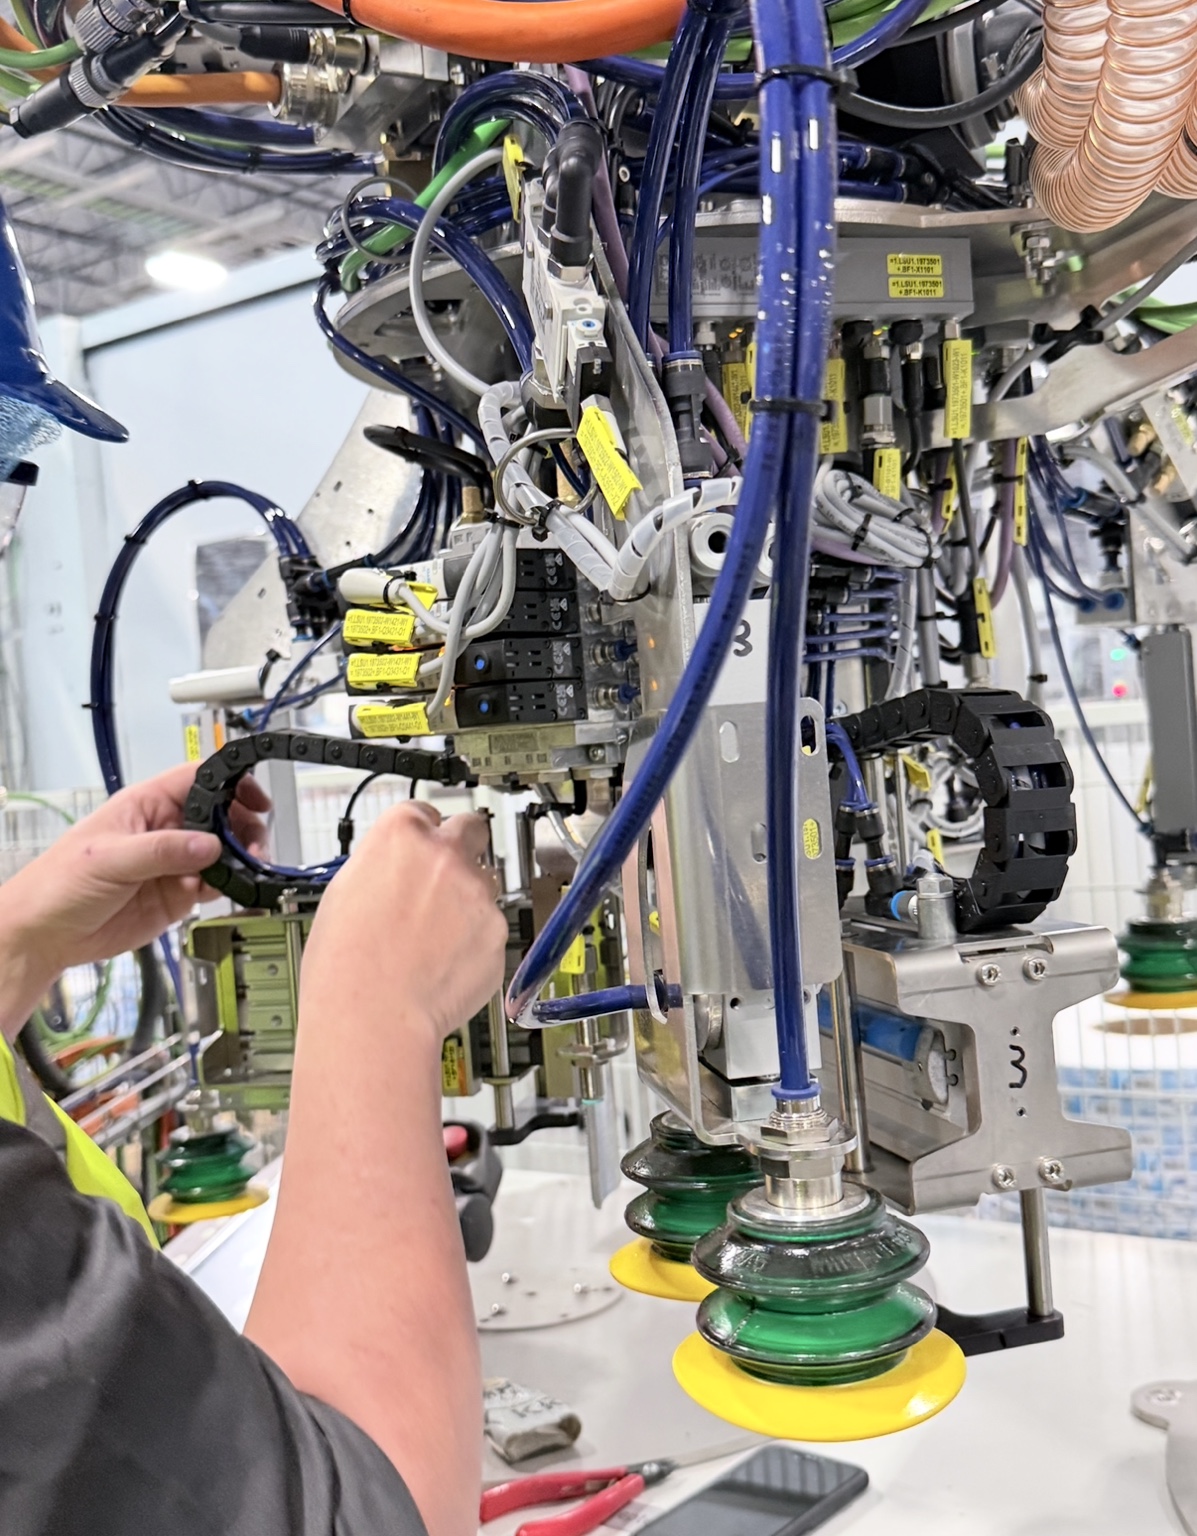
Selected field photographs provided by the founder. Shown as professional experience, not Buntop client endorsements.
BEFORE WE TALK
Yes. An assessment starts with your installed equipment, supported interfaces, operating constraints and existing ownership. The first scope can be a single line or asset.
Yes. The assessment can be a standalone engagement with a current architecture, prioritized gaps and a roadmap. A pilot is a separate decision.
We agree on the scope and deliverables before providing a proposal. Factors include the number of systems, site access, travel, interviews and validation needs.
START A CONVERSATION
Book a 30-minute discovery call about a brownfield integration, controls architecture or GxP data project.
Monday–Friday, 8 a.m.–5 p.m. Central Time.